Alumina 96% Al2O3 is the most widely used ceramic PCB substrate grade because it balances thermal conductivity (24–28 W/m·K), high dielectric strength (>10 kV/mm), and cost roughly 40–60% lower than 99.6% alumina. The remaining 4% of the composition—typically silica, magnesia, and calcia sintering aids—determines grain structure, surface finish limits, and high-frequency loss, which is why “96% alumina” from two different suppliers can behave differently in your circuit.
Key Takeaways
- 96% alumina thermal conductivity ranges from 24–28 W/m·K at 25 °C, compared to 30–35 W/m·K for 99.6% grades (per CoorsTek and Kyocera datasheets).
- The 4% glassy-phase content in 96% grades raises dielectric loss tangent (tan δ) to roughly 0.0002–0.0010 at 1 MHz versus 0.0001–0.0003 for 99.6%.
- Flexural strength of 96% alumina is typically 350–380 MPa (ASTM C1161, 4-point bend), adequate for most thick-film and DPC circuit applications.
- 96% alumina costs approximately $0.30–$0.80 per cm² in volume, making it the default grade unless your thermal or RF spec explicitly requires higher purity.
What the “96%” Actually Means
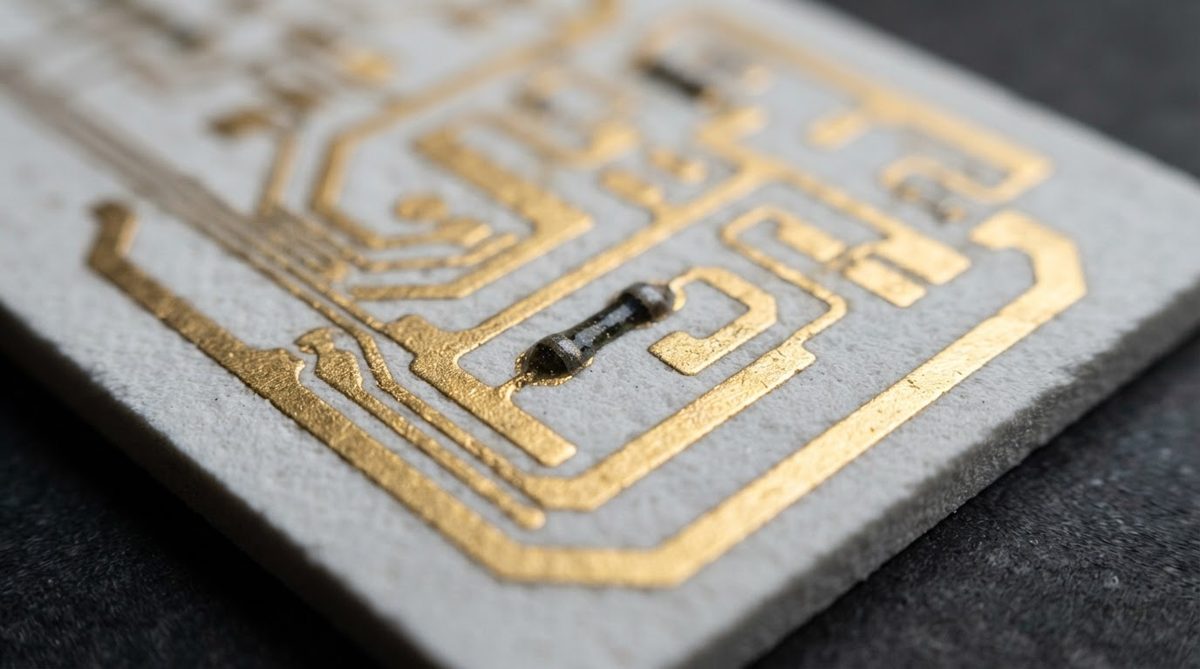
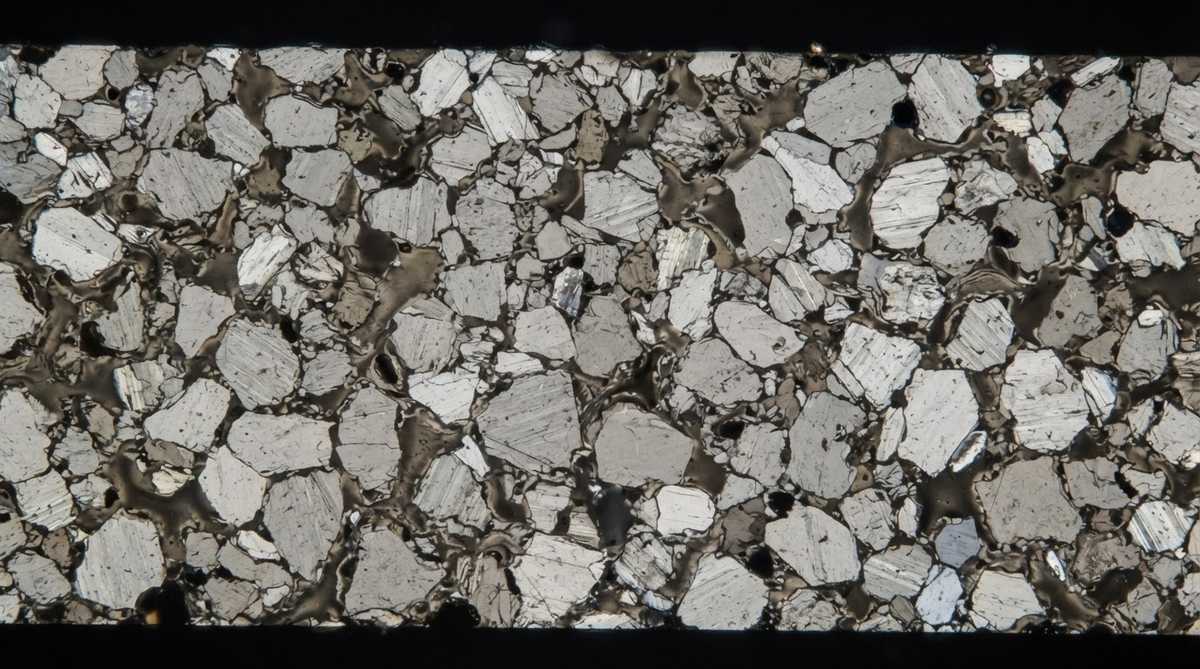
A 96% alumina substrate is 96 wt% aluminum oxide (α-Al2O3) plus 4 wt% of a sintering-aid package. Common additives include SiO2, MgO, CaO, and sometimes MnO. These form an intergranular glassy phase during firing at 1,500–1,650 °C that promotes densification and lowers the sintering temperature compared to 99.6% grades.
That glassy phase is the reason 96% alumina is cheaper to manufacture—it fires at a lower temperature and tolerates tighter dimensional control in green-state processing. It also explains every performance gap between 96% and higher-purity grades. The glass conducts heat roughly 100× worse than crystalline alumina, absorbs more RF energy, and softens at lower temperatures. For detailed property values, see the alumina 96% material properties datasheet.
How 96% Al2O3 Grades Differ Between Suppliers
Not all 96% alumina substrates are interchangeable. Suppliers like CoorsTek (ADS-96R), Kyocera (A-473), and Maruwa (HA-96-2) each use a proprietary sintering-aid recipe. The differences show up in grain size, surface roughness, and tan δ at microwave frequencies.
Grain size typically falls between 2–8 µm for 96% grades. Finer grain means smoother as-fired surfaces (Ra 0.3–0.8 µm versus 0.8–1.5 µm for coarser grain), which matters for thin-film metallization adhesion. If your design uses thick-film screen printing, grain size is less critical. For applications requiring sub-0.1 µm Ra, a polished or lapped 96% alumina substrate is the standard approach.
Supplier Grade Comparison
| Parameter | CoorsTek ADS-96R | Kyocera A-473 | Maruwa HA-96-2 | Unit | Condition |
|---|---|---|---|---|---|
| Al2O3 content | 96.0 | 96.0 | 96.0 | wt% | — |
| Density | 3.72 | 3.70 | 3.70 | g/cm³ | ASTM C373 |
| Thermal conductivity | 26 | 24 | 25 | W/m·K | 25 °C |
| Flexural strength | 379 | 350 | 360 | MPa | ASTM C1161, 4-pt bend |
| Dielectric constant (εr) | 9.4 | 9.5 | 9.4 | — | 1 MHz |
| Tan δ | 0.0002 | 0.0004 | 0.0003 | — | 1 MHz |
| Surface roughness (as-fired) | 0.5–1.0 | 0.6–1.2 | 0.4–0.8 | µm Ra | — |
| CTE | 7.4 | 7.2 | 7.3 | ppm/°C | 25–400 °C |
Typical values for commercially available material, for comparison only. Confirm against the datasheet for your specific grade.
96% vs. 99.6% Alumina: When Does Purity Matter?
The jump from 96% to 99.6% Al2O3 purity eliminates most of the glassy phase, which improves three things: thermal conductivity rises to 30–35 W/m·K, loss tangent drops below 0.0003 at 1 MHz, and the substrate survives higher continuous operating temperatures (up to 1,700 °C versus roughly 1,600 °C). For a deeper comparison, the 99.6% alumina material properties page has full datasheet values.
You pay for those gains. 99.6% substrates cost 2–3× more per piece in production quantities, and lead times are often longer because fewer suppliers stock standard sizes. The decision framework is straightforward:
- Specify 96% when thermal conductivity above 24 W/m·K is sufficient, operating frequency is below 10 GHz, and cost matters.
- Specify 99.6% when your design dissipates more than ~5 W/cm², operates above 20 GHz, or requires thin-film metallization with line/space below 50 µm.
Worked Example: Does 96% Alumina Handle Your Thermal Load?
Suppose you have a power LED module dissipating 3 W over a 10 mm × 10 mm footprint on a 0.635 mm thick substrate. The conduction thermal resistance through the substrate is:
Rth = t / (k × A) = 0.000635 m / (25 W/m·K × 0.0001 m²) = 0.254 °C/W
At 3 W, the temperature drop across the substrate is 0.76 °C. Switching to 99.6% alumina (k = 33 W/m·K) reduces that to 0.58 °C—a difference of 0.18 °C. In this case, the extra cost of 99.6% buys almost nothing. If the same 3 W were concentrated on a 3 mm × 3 mm die, the drop through 96% alumina rises to 2.82 °C, and through 99.6% it is 2.14 °C. Still manageable, but the gap starts to matter when you stack it with other thermal resistances in the path.
Alumina 96% Al2O3 Grades by Application
Different applications stress different properties of the same 96% grade. Thick-film hybrid circuits prioritize as-fired surface roughness and camber for screen-print registration. RF filter substrates need the lowest available tan δ at the operating frequency. Power substrates care most about mechanical strength and thermal-cycle reliability.
For substrates thinner than 0.38 mm, handling breakage during assembly becomes a real concern. Consult available 96% alumina thickness and tolerance options before committing to a design that pushes the mechanical limits of the material.
When Not to Use 96% Alumina
96% alumina is the wrong choice in several specific situations:
- Thermal loads above ~8 W/cm² on small die. Aluminum nitride (170–200 W/m·K) is a better fit. See the AlN grades comparison for options.
- Millimeter-wave frequencies (>30 GHz). The glassy phase in 96% alumina causes unacceptable insertion loss. Use 99.6% alumina or fused silica.
- Cost-driven consumer electronics with modest thermal needs. FR-4 or metal-core PCBs cost a fraction of ceramic and are sufficient below 130 °C and 2 W/cm².
- Large-area boards (>150 mm × 150 mm). Ceramic substrates are brittle and expensive at large sizes. Consider IMS or bonded-copper aluminum panels.
Frequently Asked Questions
Is 96% alumina food-safe or biocompatible?
96% alumina is generally considered biocompatible and is used in some medical implant components. However, the sintering aids (SiO2, CaO, MgO) vary by supplier, and you must verify compliance with your specific regulatory standard (e.g., ISO 10993) against the manufacturer’s certification for that grade.
Can I use 96% alumina for HTCC circuits?
Yes. 96% alumina is the standard substrate for high-temperature co-fired ceramic (HTCC) multilayer circuits. The sintering temperature (1,500–1,650 °C) requires tungsten or moly-manganese metallization because copper and silver would melt.
Does 96% alumina work with lead-free solder?
It does, provided the metallization and surface finish are compatible. SAC305 solder (melting at ~217 °C) wets properly to thick-film gold, nickel/gold, or silver-palladium metallization on 96% alumina. The substrate itself is unaffected by reflow temperatures up to 300 °C.
How do I tell which 96% grade a supplier actually uses?
Ask for the material trade name and the supplier’s lot-level Certificate of Analysis (CoA). Reputable substrate manufacturers (CoorsTek, Kyocera, Maruwa, CeramTec) publish datasheets keyed to a specific grade designation. If a PCB fabricator cannot tell you the substrate grade, treat that as a red flag.
What is the maximum continuous use temperature for 96% alumina?
The ceramic itself survives above 1,600 °C. The practical limit is set by the metallization: thick-film conductors are rated to 300–500 °C depending on the paste system, and solder joints fail well below that. The substrate is almost never the thermal bottleneck.