What Is HTCC? A Clear HTCC Definition
The HTCC definition in one sentence: HTCC (High-Temperature Co-Fired Ceramic) is a multilayer ceramic packaging process in which unfired (“green”) ceramic tape layers are screen-printed with refractory metal paste, stacked, laminated, and then sintered together at 1 400–1 600 °C in a reducing or inert atmosphere. The high firing temperature produces a dense, hermetic ceramic body with embedded conductors in a single thermal cycle.
Because the co-firing temperature exceeds the melting point of copper (1 085 °C) and silver (962 °C), HTCC conductors are limited to refractory metals—typically tungsten (W) or molybdenum (Mo). These metals survive the firing step but have higher electrical resistivity than copper or silver, which is the central trade-off captured in any practical HTCC definition.
Typical HTCC Materials
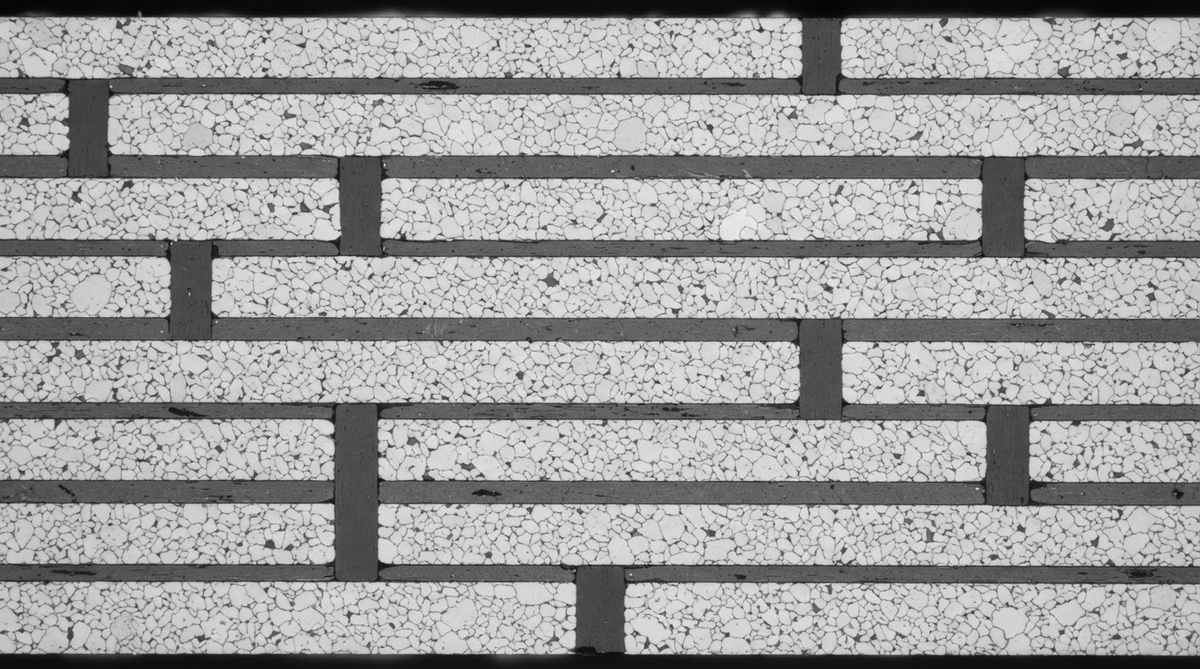
| Component | Common choices | Notes |
|---|---|---|
| Ceramic substrate | Al₂O₃ (90–96 %), AlN | AlN chosen for high thermal conductivity (170–200 W/mK) |
| Conductor paste | Tungsten (W), Molybdenum (Mo), Mo-Mn | Resistivity ~5.5 µΩ·cm (W) vs ~1.7 µΩ·cm (Cu) |
| Via fill | W or Mo paste | Vias punched or laser-drilled in green tape before firing |
| Post-fire plating | Ni/Au, Ni/Ag | Required for solderability since W and Mo are not directly solderable |
Typical values for commercially available material, for comparison only. Confirm against the datasheet for your specific grade.
HTCC Process Steps
Understanding the process flow is essential to grasping the full HTCC definition, because the sequence of operations dictates both the capabilities and the constraints of the technology.
- Tape casting — Ceramic powder, binder, and solvent are cast into thin green sheets (typically 0.1–0.6 mm).
- Via formation — Holes are punched or laser-drilled through individual sheets.
- Screen printing — W or Mo paste is printed onto each layer for traces and via fills.
- Stacking and lamination — Layers are aligned, stacked, and pressed together under heat and pressure.
- Co-firing — The laminated stack is sintered at 1 400–1 600 °C in a hydrogen or hydrogen/nitrogen atmosphere.
- Post-fire metallization — Exposed W/Mo pads are plated with Ni/Au for wire bonding or soldering.
HTCC Definition Compared to LTCC
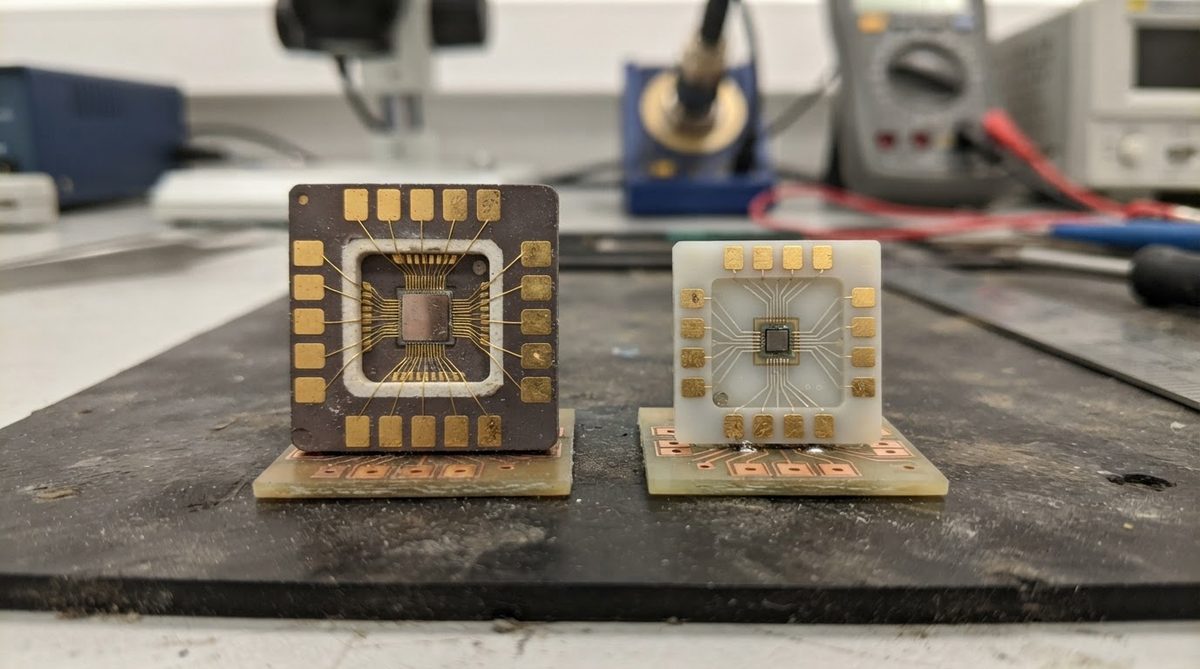
The easiest way to sharpen the HTCC definition is to contrast it with LTCC (Low-Temperature Co-Fired Ceramic). Both are multilayer co-fired processes, but they diverge on firing temperature, conductor choice, and target applications.
| Parameter | HTCC | LTCC |
|---|---|---|
| Firing temperature | 1 400–1 600 °C | 850–900 °C |
| Conductor metals | W, Mo | Ag, Au, Cu |
| Conductor resistivity | ~5.5 µΩ·cm (W) | ~1.6 µΩ·cm (Ag) |
| Ceramic body | Al₂O₃, AlN | Glass-ceramic composites |
| Hermeticity | Excellent | Good |
| RF performance | Lower (higher conductor loss) | Higher (lower loss metals, tunable Dk) |
Choose HTCC for high-temperature environments, hermetic packaging, and structural strength. Choose LTCC when low conductor loss, embedded passives, or lower-cost silver metallization matter more.
When HTCC Is Not the Right Choice
If your design is driven by RF signal integrity and low insertion loss, LTCC’s silver or gold conductors outperform tungsten significantly. For cost-sensitive, non-hermetic applications below 200 °C, standard FR-4 or metal-core PCBs are far cheaper. HTCC tooling costs are also high, so low-volume prototypes with simple single-layer geometry may be better served by DPC or thick-film processes on pre-fired substrates.
Frequently Asked Questions
What does HTCC stand for?
HTCC stands for High-Temperature Co-Fired Ceramic. The name refers to the defining characteristic of the process: multiple ceramic and conductor layers are fired together (“co-fired”) at temperatures between 1 400 °C and 1 600 °C, well above the range used in LTCC.
Why can’t copper be used in HTCC?
Copper melts at 1 085 °C, which is far below the 1 400–1 600 °C HTCC firing range. Only refractory metals like tungsten (melting point 3 422 °C) and molybdenum (2 623 °C) survive the sintering step intact. This is why the HTCC definition inherently implies tungsten or molybdenum conductors.
Is HTCC hermetic?
Yes. The high sintering temperature produces a fully dense ceramic body with helium leak rates typically below 1 × 10⁻⁸ atm·cc/s per MIL-STD-883. This hermeticity is one of the primary reasons engineers select HTCC for military, aerospace, and downhole sensor packaging.
How many layers can an HTCC package have?
Commercial HTCC packages commonly range from 2 to over 60 layers. The practical limit depends on via registration accuracy, shrinkage control during firing, and the manufacturer’s lamination capability. Complex packages for military hybrid modules routinely exceed 20 layers.