The AMB definition in one sentence: Active Metal Brazing (AMB) is a process that bonds copper foil to a ceramic substrate using a braze alloy containing an active element—almost always titanium—that reacts chemically with the ceramic surface. This direct chemical bond eliminates the need for pre-metallising the ceramic. Understanding the AMB definition matters because it is the dominant bonding method for high-reliability power-electronic substrates built on Si₃N₄ and AlN ceramics.
What Does AMB Mean? Core AMB Definition and Process
A thin foil of braze alloy (typically AgCu with 1–5 wt% Ti) is placed between the copper sheet and the ceramic. The assembly enters a vacuum furnace at 800–900 °C. At temperature, titanium migrates to the ceramic interface and reacts to form TiN (on AlN) or TiN/Ti₅Si₃ (on Si₃N₄). This reaction layer wets the ceramic and allows the molten AgCu to bond the copper firmly to it. The process is a specific form of brazing, distinguished by that reactive-metal step.
The key steps in the AMB process are:
- Layup – Copper foil, braze foil, and ceramic blank are stacked in a fixture.
- Vacuum furnace loading – The stack enters a furnace pumped to ≤ 10⁻³ Pa to prevent oxidation of the titanium.
- Heating to 800–900 °C – The braze alloy melts; titanium diffuses to the ceramic surface and reacts.
- Cooling under controlled profile – Slow cooling minimises residual stress from the CTE mismatch between copper and ceramic.
- Etching and finishing – The bonded panel is patterned by photolithography and etched to form circuit traces.
AMB vs. DBC: How the AMB Definition Differs from Direct Bond Copper
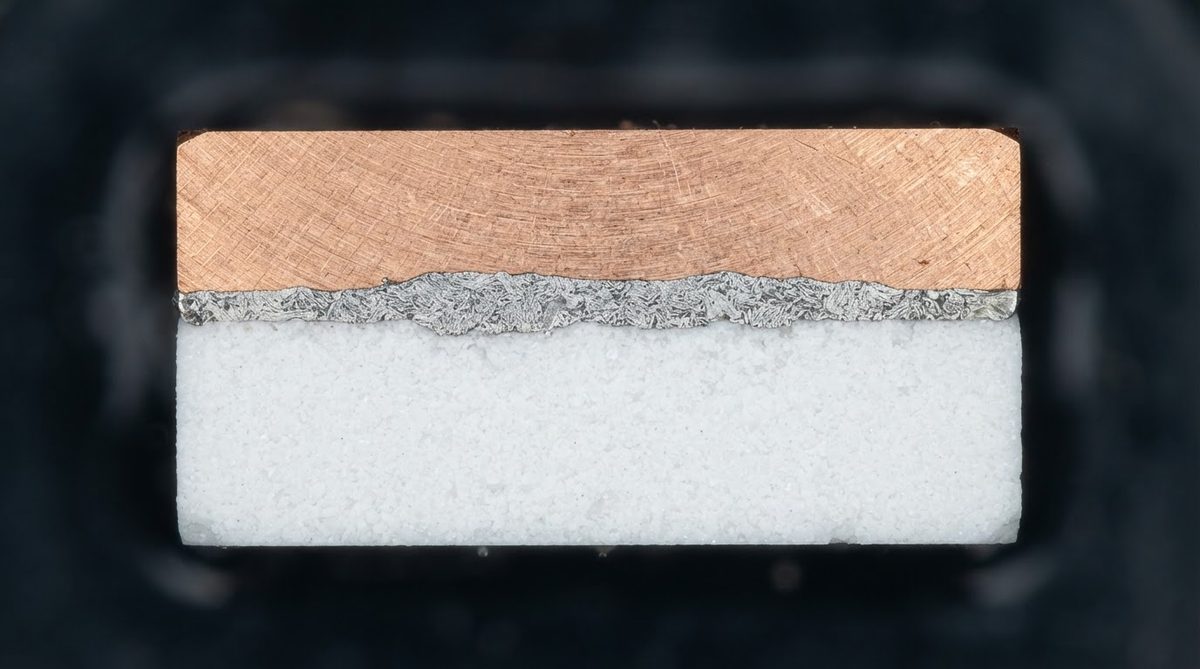
AMB is often compared to DBC (Direct Bond Copper). DBC relies on a copper-oxide eutectic to bond copper to Al₂O₃ or AlN at roughly 1 065 °C. AMB operates at a lower peak temperature and works with Si₃N₄, which DBC cannot bond reliably. AMB also permits thicker copper (up to 0.8 mm is common; 1.2 mm is possible) because the ductile braze layer absorbs CTE mismatch stress better than the brittle DBC interface.
| Parameter | AMB | DBC |
|---|---|---|
| Peak process temperature | 800–900 °C | ~1 065 °C |
| Typical copper thickness | 0.3–0.8 mm | 0.2–0.4 mm |
| Compatible ceramics | Si₃N₄, AlN, Al₂O₃ | Al₂O₃, AlN |
| Thermal-cycle reliability (–40/+150 °C) | >3 000 cycles typical | ~1 000 cycles typical |
Typical values from published Kyocera and Rogers curamik datasheets, for comparison only. Confirm against the datasheet for your specific grade.
Where AMB Substrates Are Used
AMB substrates dominate in high-reliability power electronics: EV traction inverters, railway converters, wind-turbine power modules, and industrial motor drives. The combination of Si₃N₄ ceramic (flexural strength 600–800 MPa per ASTM C1161) with thick copper gives these modules the thermal-cycling endurance that automotive and rail qualification standards demand.
Enter your substrate material, copper thickness, and target cycle count below to see estimated temperature derating for your design.
When AMB Is Not the Right Choice
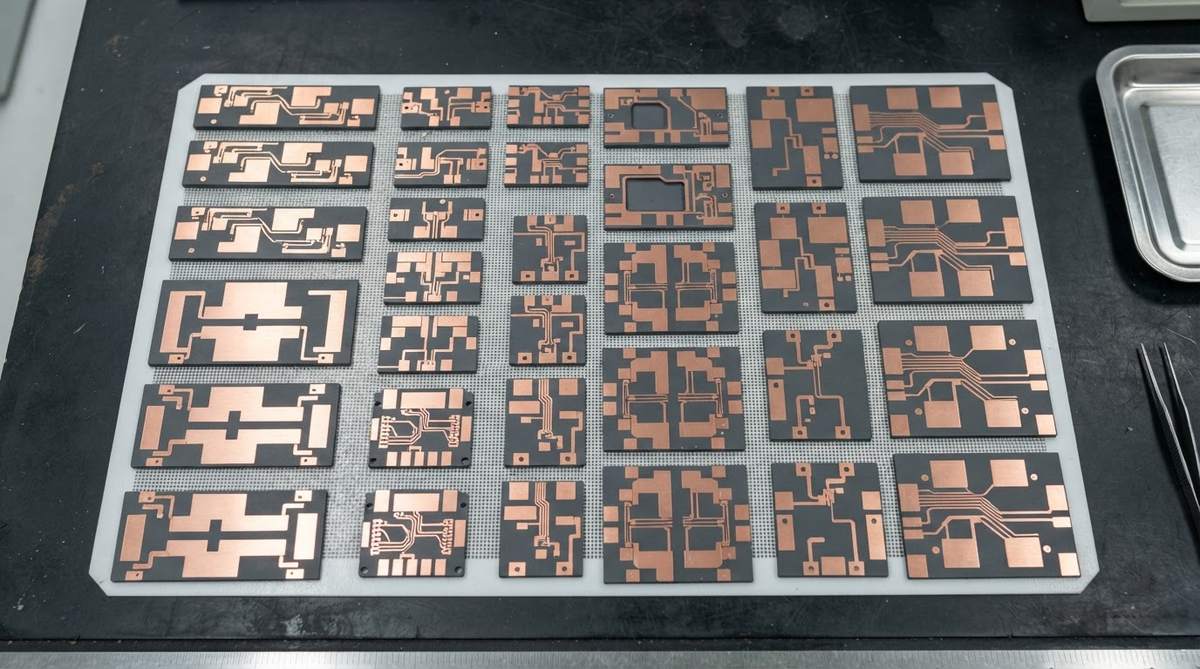
AMB substrates cost significantly more than DBC or standard Al₂O₃ boards. If your application does not require extreme thermal cycling, thick copper, or Si₃N₄, a DBC on 96% alumina or an LTCC multilayer may be a better fit at a fraction of the price. AMB also has longer lead times due to vacuum-furnace batch processing.
Frequently Asked Questions
Is AMB the same as active metal brazing?
Yes. AMB is simply the abbreviation for Active Metal Brazing. The AMB definition refers specifically to the use of a titanium-containing braze alloy to create a reactive bond between copper and ceramic in a vacuum furnace at 800–900 °C.
Can AMB bond any ceramic material?
AMB bonds Si₃N₄, AlN, and Al₂O₃ reliably. It is the only proven production method for bonding copper to Si₃N₄. DBC, by contrast, is limited to Al₂O₃ and AlN. ZrO₂ and BeO are not standard AMB substrates.
Why is AMB more expensive than DBC?
AMB requires a high-vacuum furnace, a precious-metal braze alloy (silver-copper-titanium), and slower batch processing. These factors raise per-unit cost by roughly 2–4× compared to DBC on alumina, depending on volume and copper thickness.
What copper thickness can AMB achieve?
Standard AMB production supports 0.3–0.8 mm copper. Some suppliers offer up to 1.2 mm. Thicker copper increases current-carrying capacity and heat spreading but also increases residual stress, so substrate design must account for warpage and edge-crack risk.